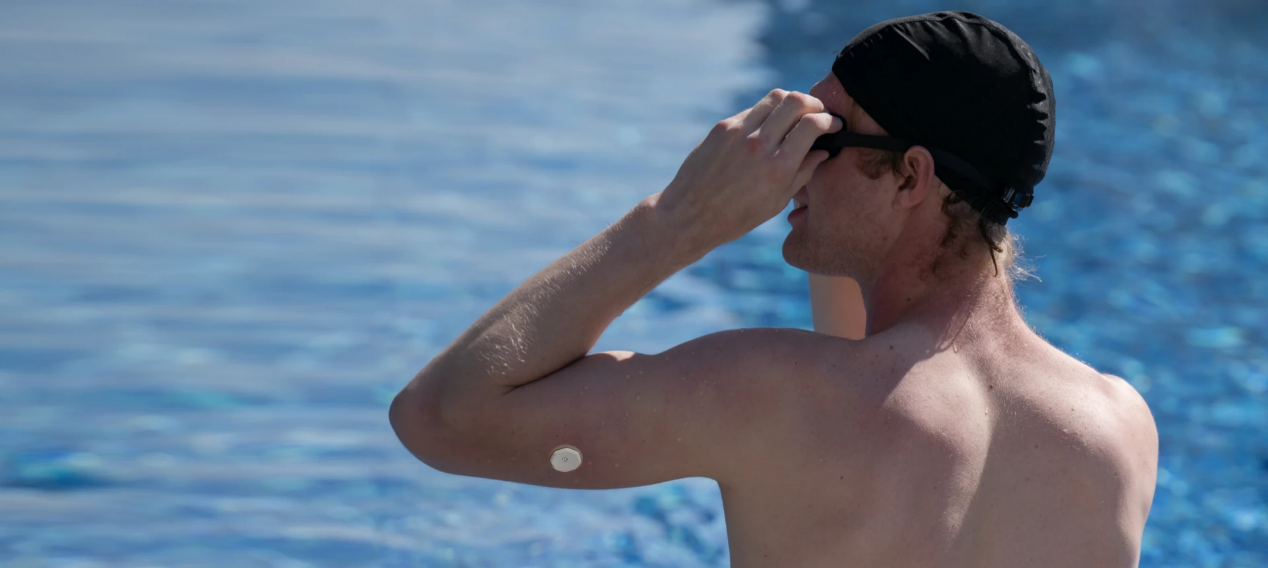
As CGM moves into broader everyday use, manufacturers must keep product performance consistent while increasing output. High-volume production puts pressure on sourcing, assembly, testing, packaging, software, and traceability, so quality depends on connected controls rather than final inspection alone. For buyers assessing a CGM system, the production discipline behind products such as iCan CGM can be as important as the specifications listed on the package.
Turn Design Requirements into Production Controls
Quality at scale begins before a sensor reaches the production line. Manufacturers need defined specifications for sensing components, electronics, adhesives, packaging, and software, together with procedures showing how each requirement will be verified.
ISO 13485:2016 is a major reference for medical-device quality management. ISO describes it as a standard for organizations involved in medical-device design and manufacture, and the 2016 edition was reviewed and confirmed in 2025. In the United States, the FDA’s Quality Management System Regulation became effective on February 2, 2026incorporating ISO13485:2016 by reference while retaining certain FDA-specific requirements.
For high-volume production, design requirements should become measurable acceptance criteria that remain visible during routine manufacturing.
Control Materials Before Assembly
A production line can only be as consistent as its inputs. CGM manufacturing relies on sensing materials, electronic components, adhesives, batteries, packaging, and other specialized parts. Variation in a critical component can affect performance even when the assembly process has not changed.
Supplier qualifications and incoming inspection help control this risk. Manufacturers can set specifications for critical materials, assess supplier performance, inspect incoming lots, and retain records for traceability. Changes to materials or suppliers should also pass through formal change control when they may affect device performance.
Use In-Process Testing
Final inspection can identify defective units, but high-volume production benefits from checkpoints throughout manufacturing.
Automated equipment can monitor dimensions, assembly conditions, electrical characteristics, or other defined parameters, while operators verify steps requiring additional judgment. Process monitoring can help detect drift before a small problem becomes a large batch of nonconforming products.
This matters because a CGM combines sensing, electronics, communication, and software functions. Hardware and software defects may require different verification and release controls rather than relying on final inspection alone.
Verify Critical Performance with Consistent Methods
Performance claims need supporting test methods and context. MARD is widely used in CGM evaluation, but results can vary with reference methods, study populations, sensor placement, wear duration, and other conditions. CLSI POCT05 Ed2 addresses point accuracy, trend accuracy, alerts, system stability and reliability, clinical studies, calibration, traceability, cybersecurity, and labeling.
The iCan i6 specifications report an overall adult MARD of 8.71%, a 15-day sensor life, and glucose readings every three minutes. It also lists a 2.0–25.0 mmol/L monitoring range and IP28 protection. These specifications define important product characteristics that manufacturers need to maintain through controlled production and verification processes as output increases.
Maintain Traceability Across Large Batches
As output grows, traceability becomes increasingly important. Production batches should be linked to relevant materials, manufacturing records, inspection results, and release information. This enables quality teams to determine which products may have been affected when an issue is discovered.
Traceability also supports corrective action. If a recurring complaint appears after distribution, batch records can help investigators identify the cause and define the scope of potentially affected products.
Buyers should ask whether lot information can be traced consistently through manufacturing, release, distribution, and complaint handling.
Manage Software and Manufacturing Changes
Connected CGM systems add software to the quality equation. Updates to apps, firmware, algorithms, alerts, or data handling can influence the user experience and should be assessed through controlled development and release procedures.
Manufacturing changes also require discipline. Equipment may be replaced, suppliers may change, packaging may be updated, or new capacity may be added. Each change needs an evaluation to determine whether verification or validation is required.
Sinocare states that it has nine global R&D and manufacturing sites and a presence in 187 countries and regions. Such infrastructure provides organizational context, while specific manufacturing controls still need to be verified for the device and site being considered.
Scale Output Without Losing Stability
Increasing production can reveal weaknesses that are less visible at smaller volumes. Additional shifts, operators, equipment, or suppliers may alter conditions under which a process was originally validated.
Controlled expansion is therefore important. Manufacturers can qualify new lines, standardize operator training, compare equipment performance, and monitor key process indicators during ramp-up. Capacity planning should also include maintenance, calibration, environmental controls, and contingency arrangements instead of focusing only on nominal output.
For continuous glucose monitoring device manufacturers, the ability to increase production while retaining consistent performance is an important part of commercial readiness. Buyers should ask how capacity expansions are validated and how quality data are compared before and after a change.
Connect Quality with the Product Lifecycle
Effective high-volume CGM production works as a continuous loop: qualified materials enter controlled processes, testing confirms performance, production data reveal variation, traceability supports investigation, and post-market feedback informs improvement.
The iCan i6 provides one example of a CGM system built around continuous readings and connected data. Sinocare’s stated R&D and manufacturing footprint adds context to its broader capabilities, while the actual quality of each device depends on the controls applied throughout its lifecycle.
What Consistent Quality Looks Like at Scale
High-volume CGM manufacturing is not simply about producing more units per day. Consistency comes from controlling critical inputs, monitoring production steps, validating changes, maintaining traceability, and using reliable methods to verify performance.
Sinocare’s experience in glucose-management products provides a relevant example of a broader medical-device organization operating across R&D and manufacturing. Procurement teams can examine quality-system documentation, lot traceability, performance evidence, change-control procedures, and production-scale validation together.